

 EU
What is a CNC Machine?
CNC stands for computer numerical control. A CNC machine follows a written program to move a cutting tool, a workpiece, or both. The program is usually G-code with M-code. G-code describes motion, such as where to go and how fast. M-code switches machine functions, such as spindle start and coolant on.
The path from design to part is short. A designer builds a 3D model in CAD. CAM software turns the model into toolpaths and exports them as a program, forming the basis of CNC programming from design to code. The controller reads that program line by line and sends commands to the motors. Sensors report back, and the controller corrects any error. The spindle cuts, coolant clears heat and chips, and the finished part comes off the CNC machine.
Every step in that machining process depends on a physical component. Knowing those components helps engineers and buyers read a quote, judge a supplier’s equipment, and design parts that machine well. It explains why two machines with the same travel can hold different tolerances. It also explains why a long, thin shaft costs more than a short, stubby one. Teams that understand them turn out high quality parts more often, and with fewer surprises.
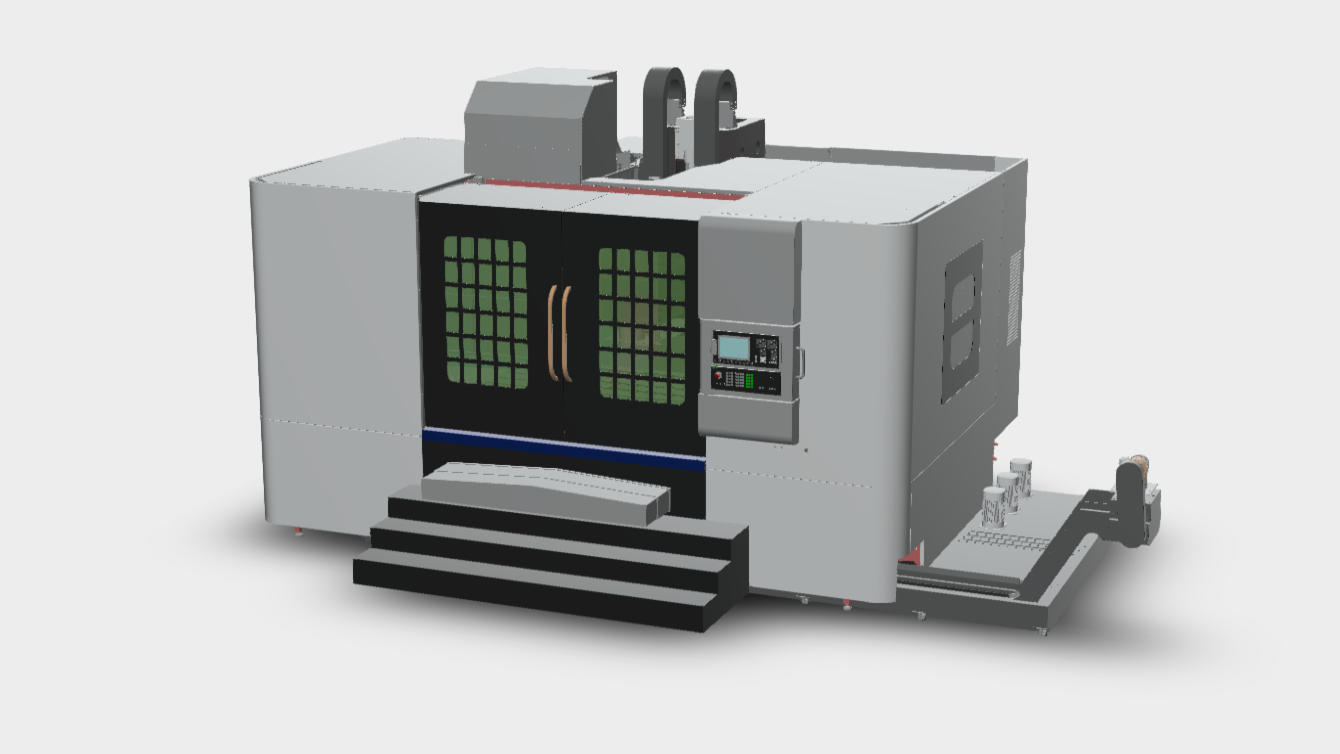
The Different Components of a CNC Machine
A CNC machine is a set of parts that each do one job. Some read the program and check the result. Others move the axes, hold the part, and make the cut. Most CNC machine parts fall into one of these roles, and a fault in one often shows up as a symptom in another. Each part has its own functions, and those functions affect precision, finish, or cycle time in any CNC manufacturing setup. Computer numerical control depends on many components working as a set.
The sections below start with the control system. They then cover the mechanical systems that move, hold, and cut the part. A table at the end sums up the key parts.
Control System
The control system is where the program meets the CNC machine. It takes in instructions, decides what every axis should do, and shows the operator what is happening. Operators work with it all day, so a clear layout matters. On a CNC milling machine, it also coordinates the X, Y, and Z axes with the cutter.
Input device
The input device loads the program. Today that usually means a USB port or a network link to a CAM computer. Older machines used punched tape and later serial connections. Whatever the method, the controller needs complete and clean instructions before a cycle can start. Clean instructions are essential, because one bad line can stop a cycle.
Machine control unit (MCU)
The MCU is the machine’s brain. Its job is converting program lines into coordinated axis moves. It reads the program, calculates how the axes must move together, and sends commands to the drives. That coordination is called interpolation. It is why a CNC machine can cut a smooth arc or a clean diagonal instead of a series of small steps. A fast MCU also keeps movement smooth at high speeds, when the program holds thousands of tiny moves.
Control panel
The control panel holds the buttons, switches, and overrides that operators use every day. These include cycle start, feed hold, spindle and feed override, and mode selection. On most modern machines the control panel is built into one console with the display.
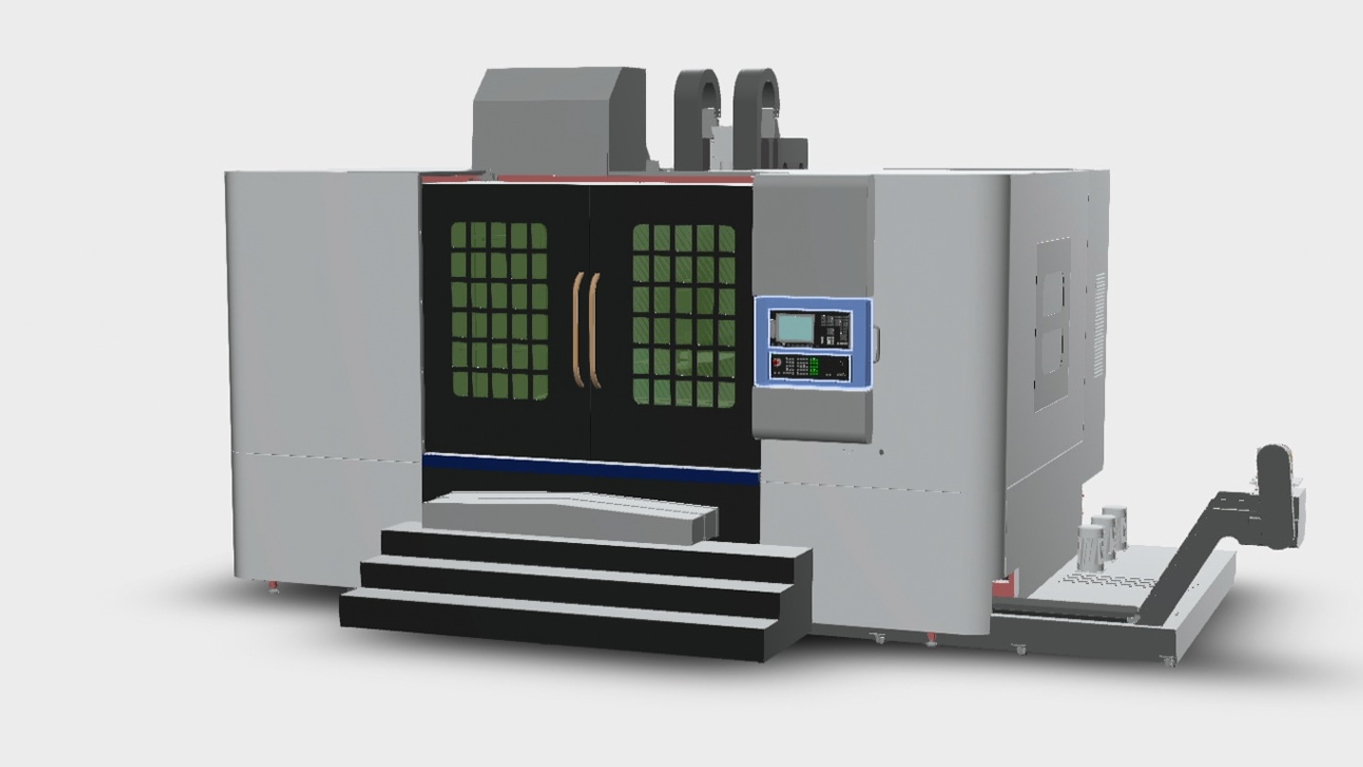
Display unit
The display unit shows axis positions, the active program, tool data, and alarms. A clear display helps operators catch a problem before it turns into scrap.
Feedback system
A feedback system is what separates a CNC machine from a motorized fixture. Sensors tell the controller where each axis really is. Without a feedback system, precision is a guess. Feedback comes in many forms, from simple switches to high-resolution scales. In closed-loop control, the controller compares the commanded position with the real one and corrects the difference.
Machine System
The systems in this group handle movement, structure, and tooling. Together they make up the core mechanical systems of a CNC machine.
Drive and Motion
The drive and motion system turns controller commands into movement. Its components set how fast a CNC machine can move. They also set how well it holds position and how much force it can apply during machining operations, whether the machine is configured for CNC milling or CNC turning.
Servo motors are the standard choice for cutting metal on a CNC machine. A servo motor works with an encoder that reports shaft position, so the drive can hold the commanded position and speed. The drive does this by converting electrical current into torque. Stepper motors are simpler and suit light-duty machines, but they can skip steps under load. Ball screws and linear guideways then turn that motor motion into straight-line travel.
Frame and column
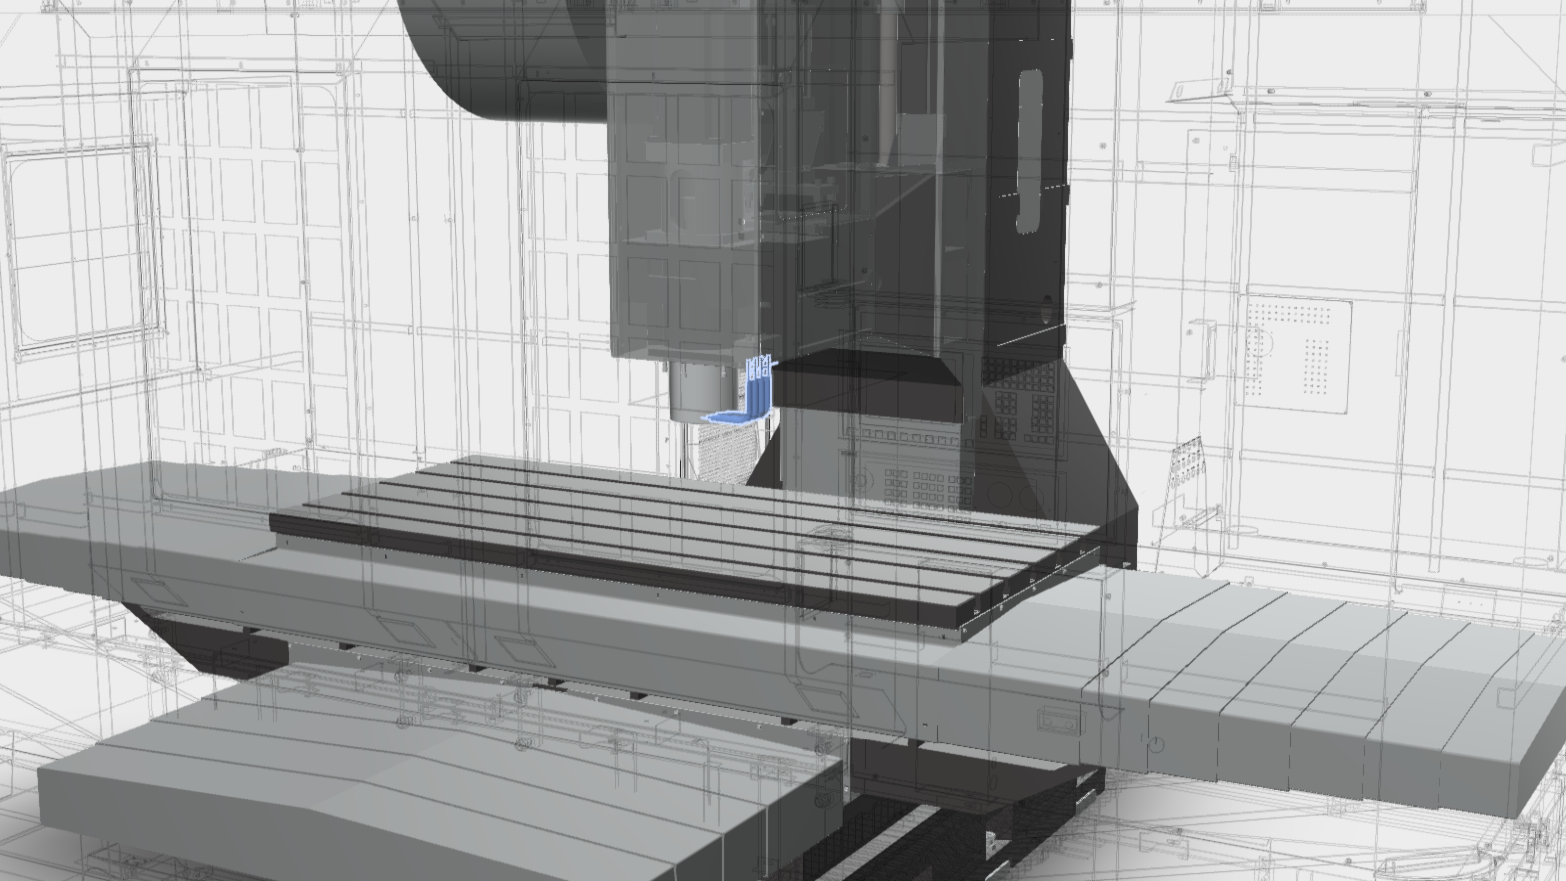
The frame and column carry the cutting head on vertical milling machines and tie it to the machine bed. Common layouts include the C-frame column on vertical machining centers, and gantry or bridge designs on larger machines and routers. Picture the force path as a loop: tool, holder, spindle, head, column, bed, table, fixture, part. Cutting force from heavy operations pushes on the whole loop, and the weakest link deflects first. A stiff column helps only if everything else in the loop is also stiff.
Heat changes structure too. Motors, bearings, and cutting all add heat, and metal grows as it warms. This is why many shops run a warm-up cycle before cutting precision parts.
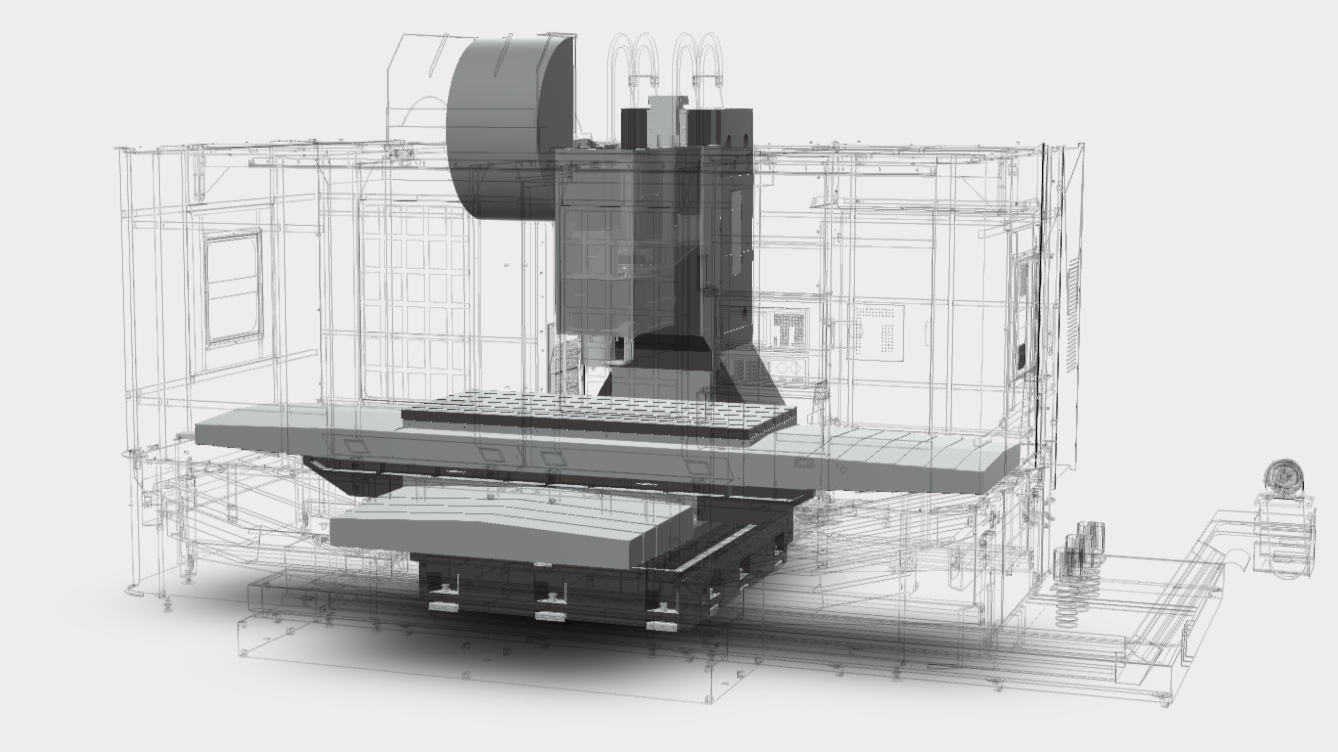
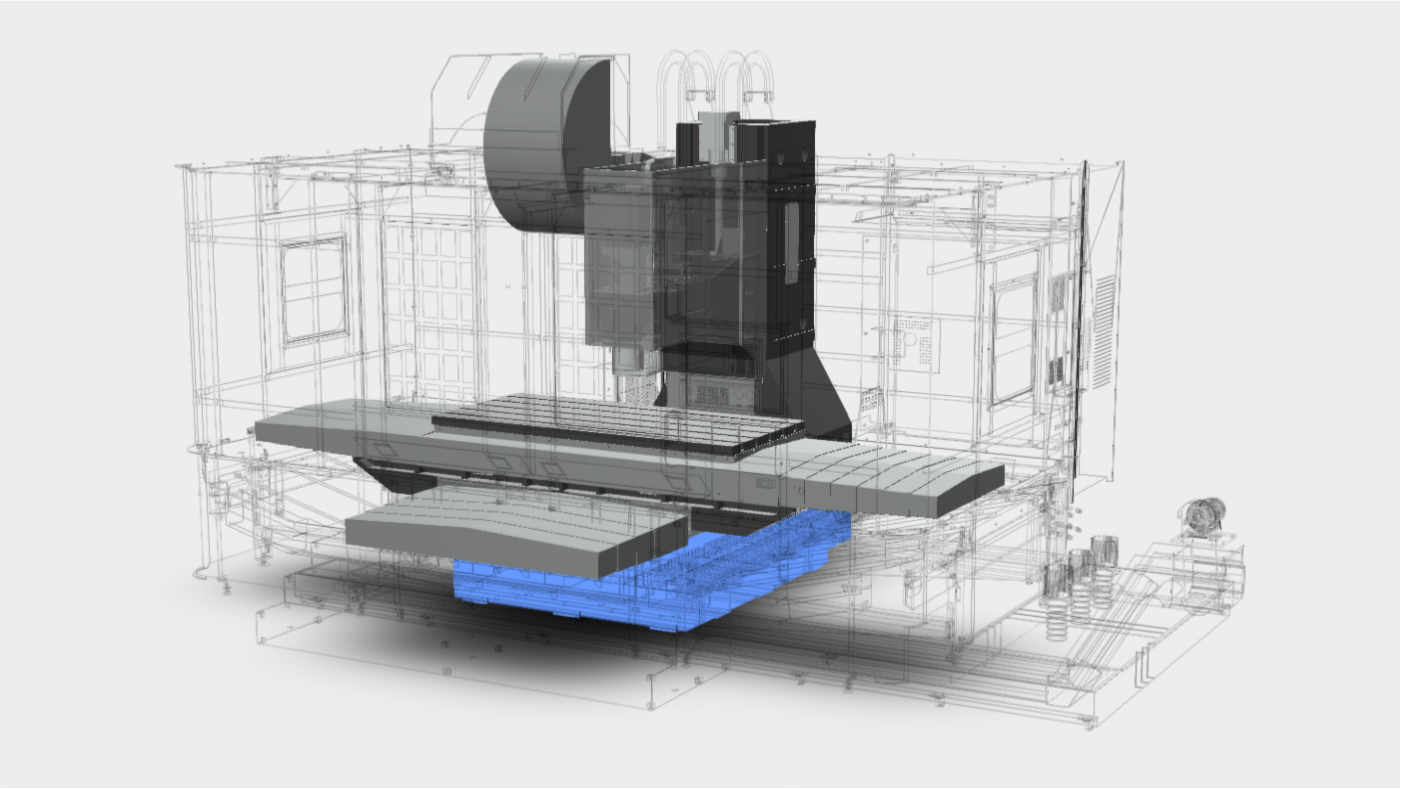
Bed
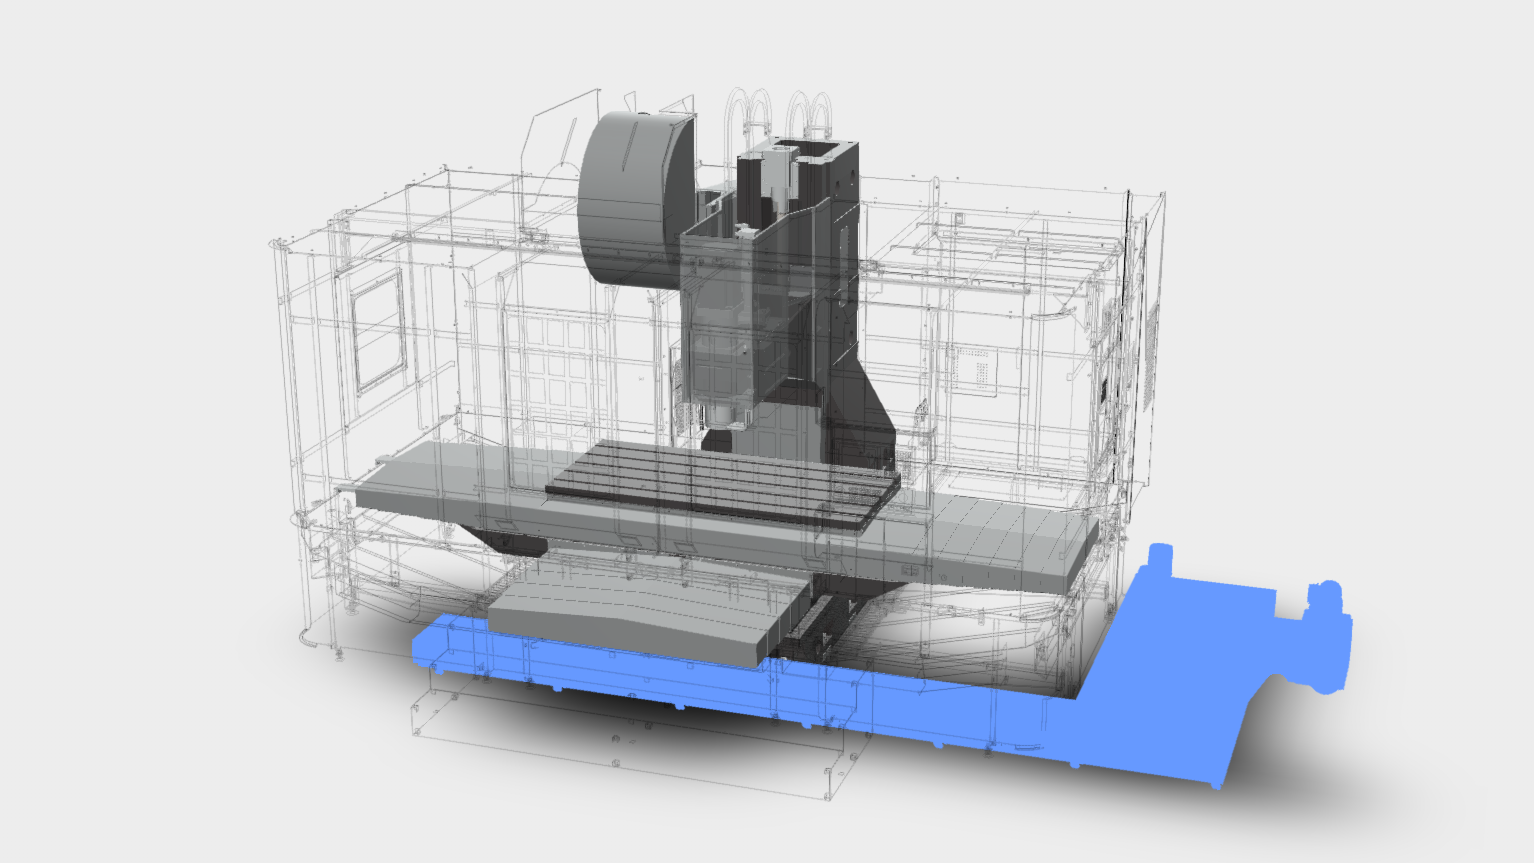
The bed, also called the machine bed, is the foundation. The axes, table, and spindle all sit on it or hang from it. A rigid bed has a critical role in accuracy and precision, because every cut passes through it. It also lets the CNC machine operate at full speed without vibration. Structural components like the bed carry every other part. On large milling machines, the machine bed is often cast iron or welded steel.
Material choice matters here, as it does for most structural components. Gray cast iron is common because it damps vibration well. Welded steel is also used, especially on large machines. Mineral casting is also called polymer concrete. It damps vibration well and stays stable as temperatures change. It appears on precision machines. A bed that lacks stiffness or damping lets cutting vibration reach the part, and the result is chatter marks.
Workholding
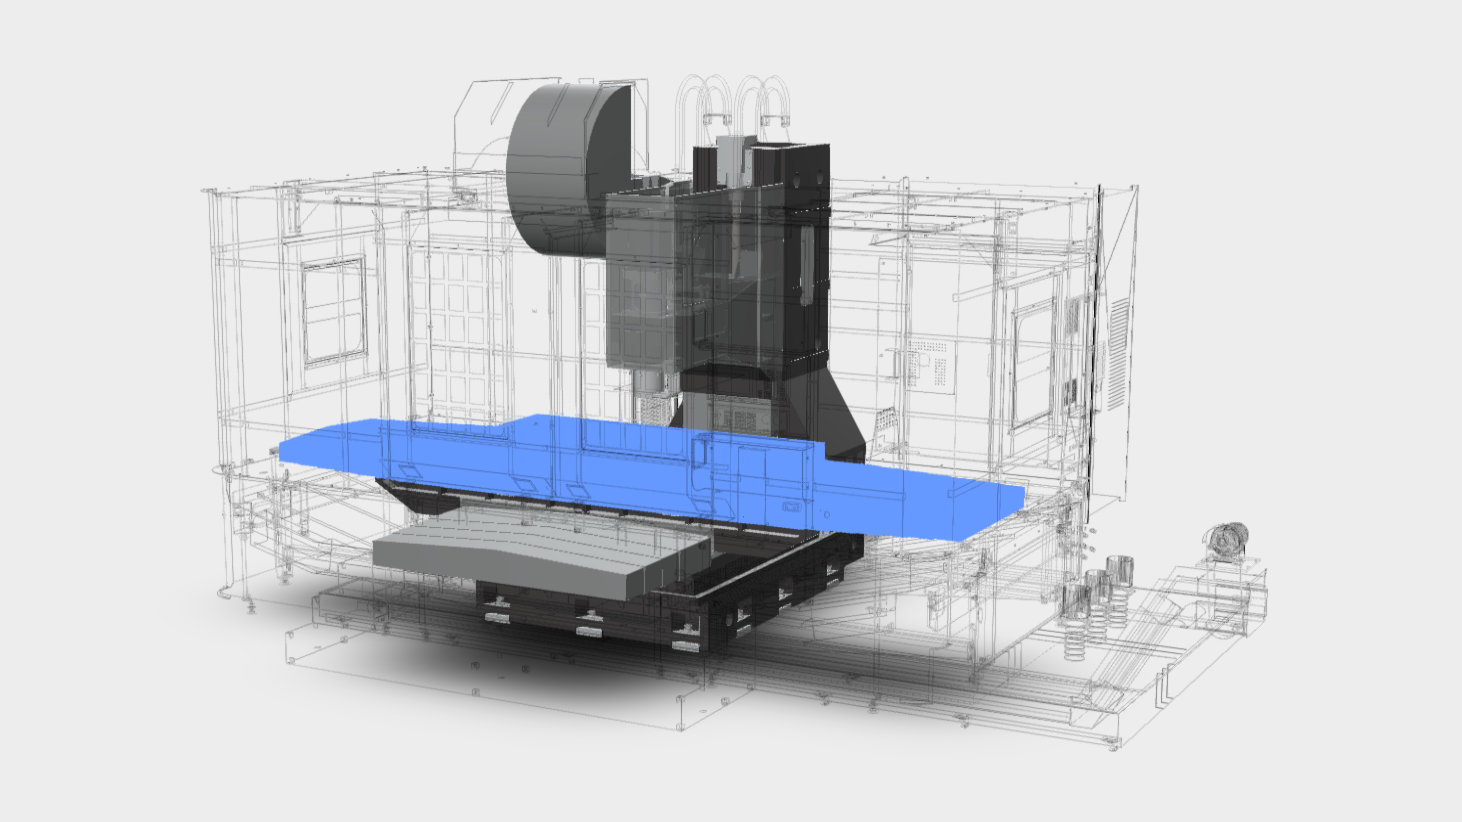
A part can only be machined as accurately as it is held. Workholding covers everything that grips, supports, or positions the workpiece. Rigid clamping is essential for thin parts. Good workholding gives repeatable quality and makes premium parts possible on an ordinary CNC machine.
Workholding components such as chucks, vises, and fixtures hold parts on both lathes and milling machines. On a CNC milling machine, vises and fixtures do the work that chucks do on a lathe. A fixture is a custom holder built for one part. It needs money up front, but it shortens setup and raises efficiency, because a machine can cut several parts in one job.
Headstock
The headstock sits at the left end of a lathe. It houses the main spindle, its bearings, and the drive, and the chuck mounts on it. Its alignment sets the baseline for every turned diameter. The headstock and tailstock are the main lathe components.
Spindle
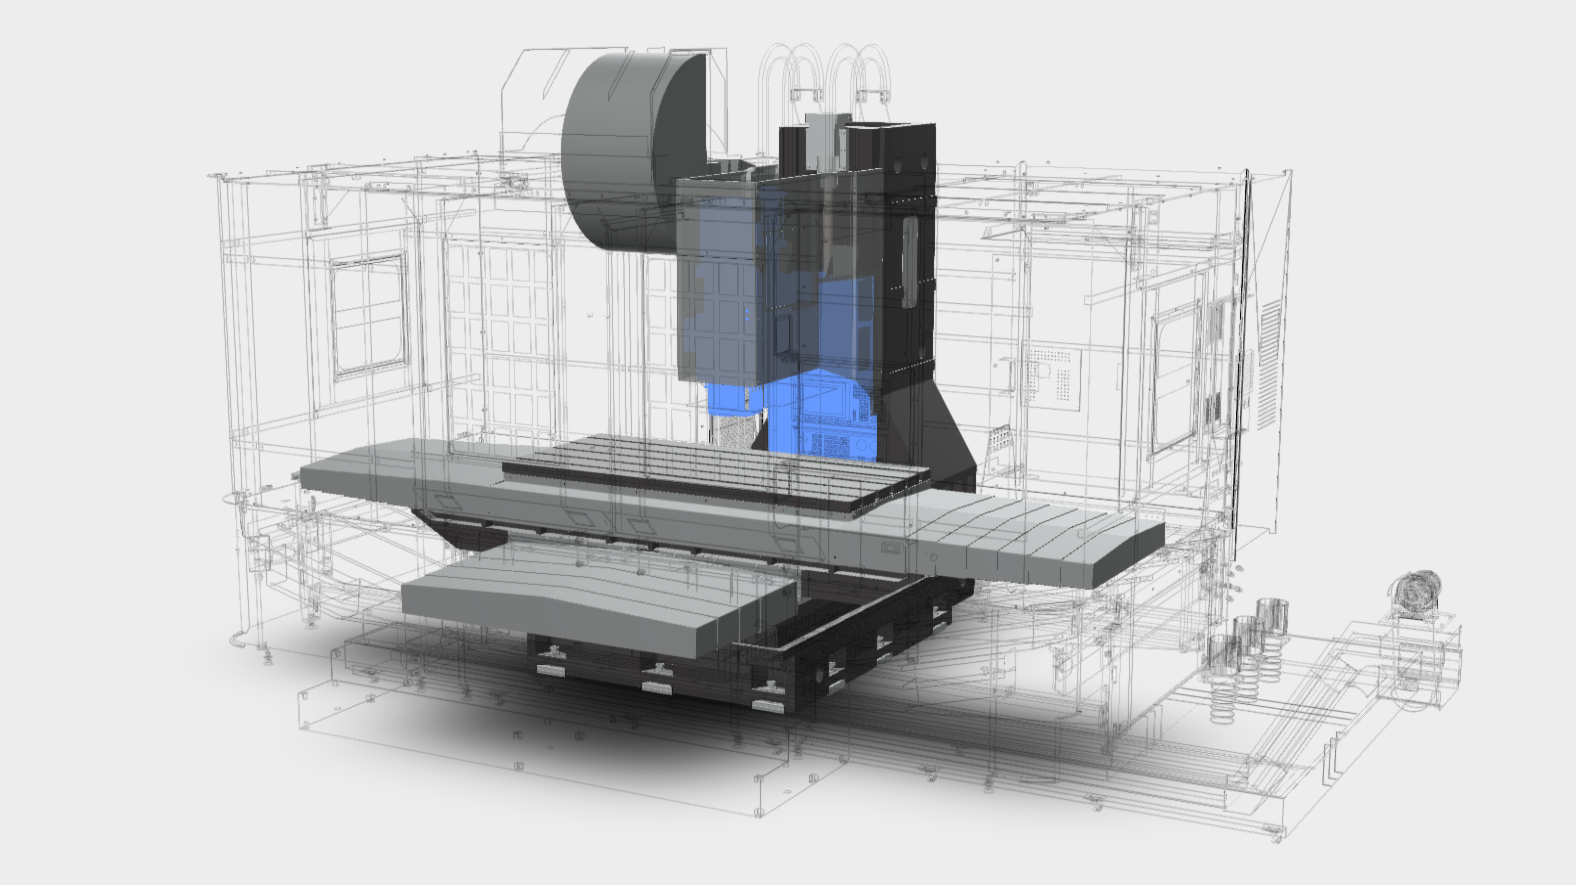
On a CNC milling machine, the spindle rotates the cutter. The spindle’s bearings, speed range, and torque set what the CNC machine can cut. Three drive styles are common.
Belt-driven spindles connect the motor to the shaft through a belt. They run quietly, are cheaper, and keep motor heat and vibration away from the cut. Their speed range is limited.
Direct-drive spindles couple the motor straight to the shaft, or build the motor into it. With no belt to wear, they run smoothly at high speed and suit finishing operations. Built-in motor designs are harder to repair.
Gear-driven spindles use a gearbox to multiply torque at low speed. They handle heavy machining operations such as roughing in steel and tough alloys, and they cut tough materials with the least strain. The gearbox adds noise and maintenance.
Cutting tools
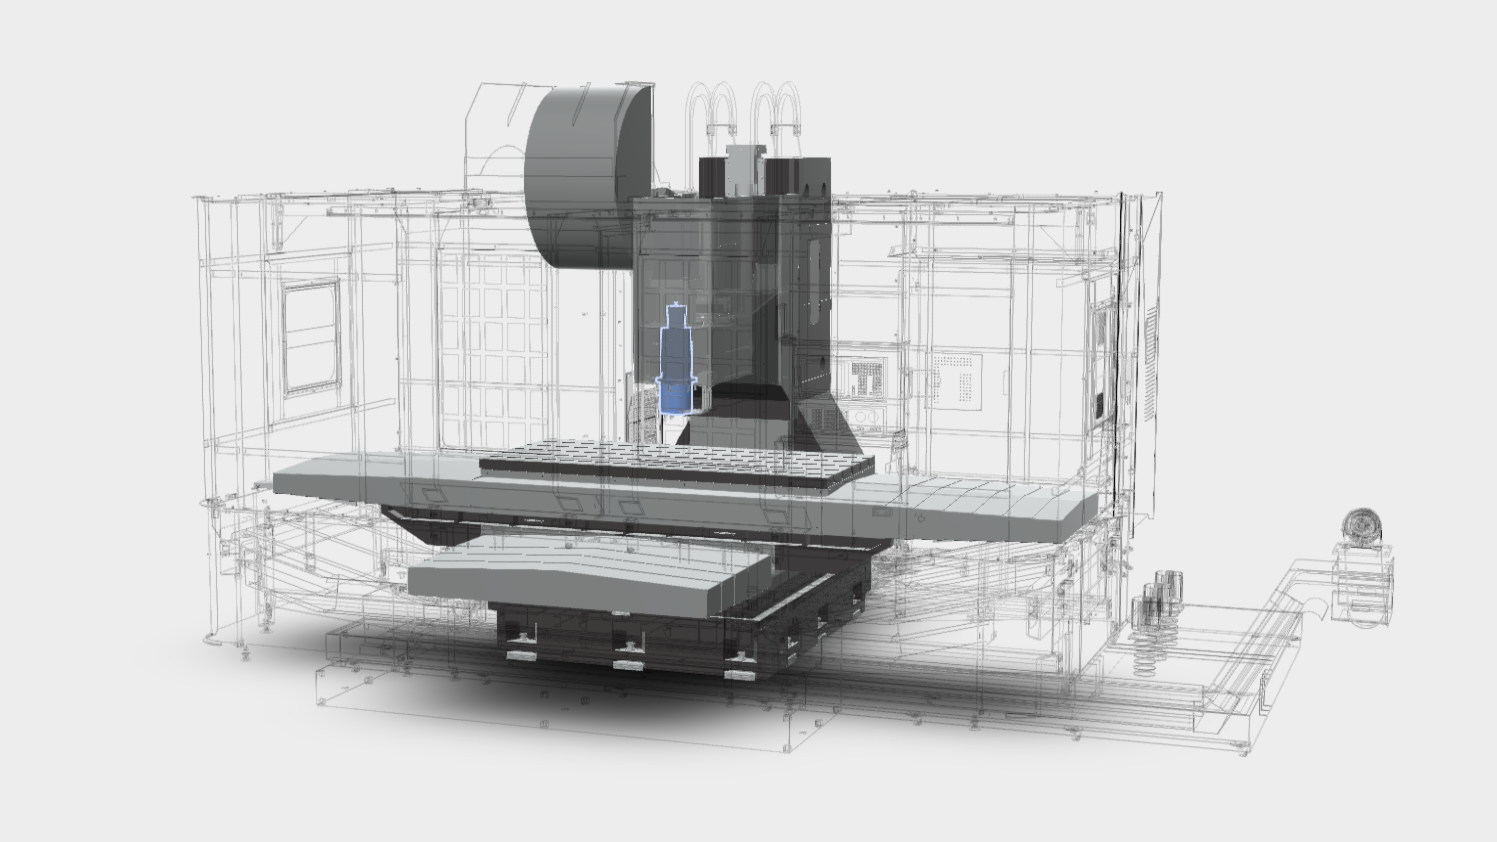
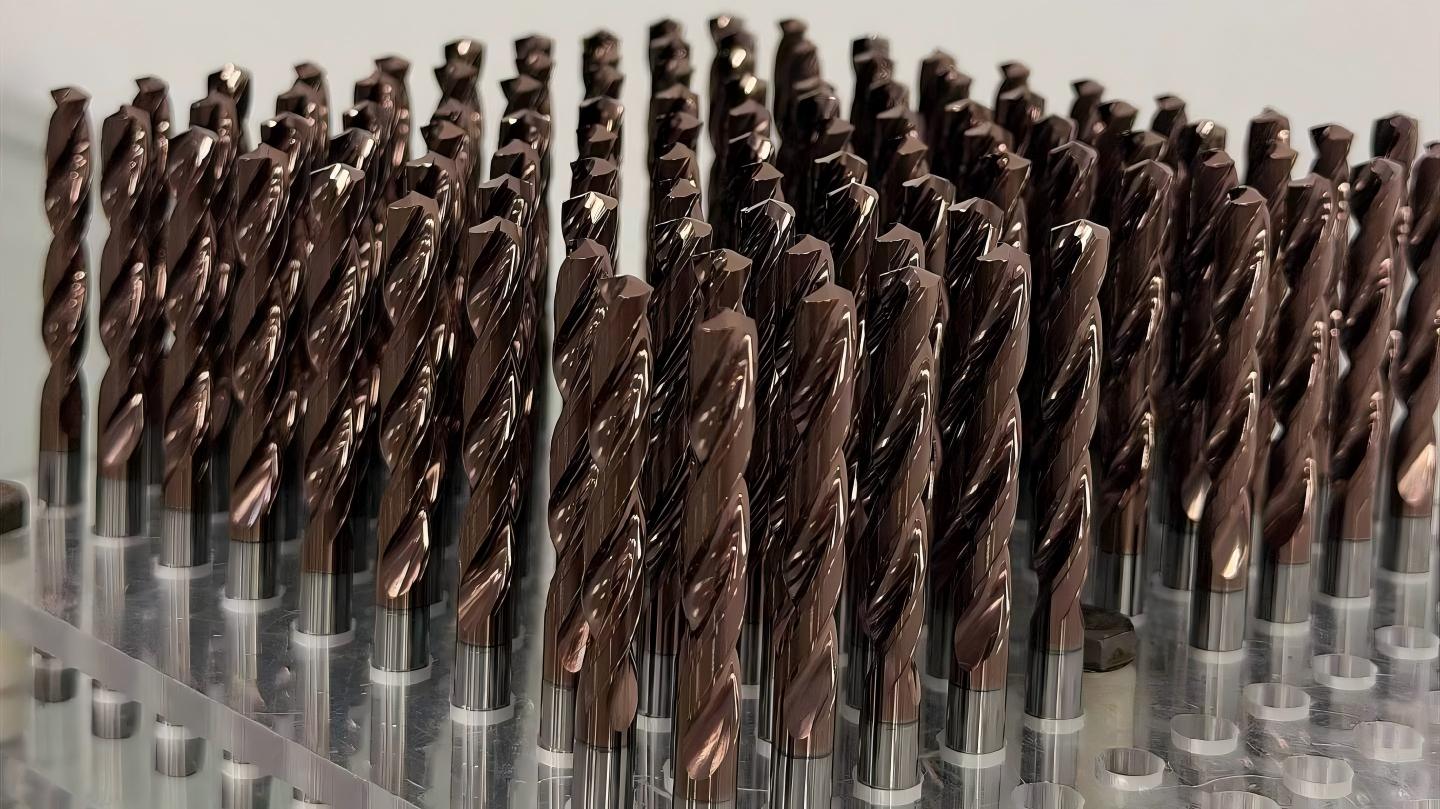
Cutting tools do the actual removal. On mills these are end mills, drills, taps, and boring bars. On lathes they are turning inserts and grooving tools. Material, shape, and geometry matter more than brand. Different materials call for different tools. An automatic tool changer (ATC) swaps the cutting tool in the spindle with one from the magazine. This cuts idle time, improves efficiency, and lets one setup finish the whole job with drilling, tapping, and milling operations. Carbide and coated tools often run faster and last longer in steel. Sharp tools with polished flutes work better in aluminum and plastics. The cutting tool you choose affects surface finish, tolerance, and cycle time.
Tailstock
The tailstock sits at the opposite end of the lathe and slides along the bed. It supports the free end of a long workpiece with a center, which reduces deflection and keeps the part straight under the tool.
Coolant system
The coolant system do not cut metal, but a CNC machine runs poorly without them. The coolant system removes heat, flushes chips, and lubricates the cut, which keeps the cutting process stable.
Flood coolant bathes the cutting zone in liquid and works well for general machining.
Mist systems spray a fine fog of coolant or lubricant in air. They use less fluid and leave cleaner parts, but they cool less.
Through-spindle coolant is delivered through the tool itself. It reaches deep holes and pockets where chips tend to pack, and it helps in tough materials. Good coolant delivery extends tool life, improves finish quality, and lets a machine operate longer between tool changes. Coolant flow is essential in deep pockets.
Chip conveyor
The chip conveyor moves chips out of the CNC machine and into a bin. A clean work area improves reliability. Chips left in the work area get recut, scratch surfaces, and add heat to the part. These small components protect finish quality.
Critical CNC Machine Components and How They Affect Quality
The table below lists the CNC machine parts that matter most for part quality. It shows what each one does and how its functions affect precision, finish, and cycle time in the machining process. The last column names the CNC manufacturing setups where each component is most common.
| Feature | Use | Impact on Output | Machine |
|---|---|---|---|
| Machine control unit | Reads the program and sends commands to the drives | Sets path accuracy and keeps motion smooth | CNC milling machines, lathes, routers |
| Servo motors | Move each axis and hold its position | Affect speed, precision, and repeatability | CNC milling machines, lathes |
| Machine bed | Supports the axes, table, and spindle | Damps vibration and protects part quality | All CNC machines |
| Spindle | Rotates the cutting tool or the workpiece | Controls surface finish, speed, and the range of materials | CNC milling machines, turning centers |
| Cutting tools | Remove material from the workpiece | Decide finish, tolerance, and cycle time | All CNC machines |
| Automatic tool changer | Swaps tools during the program | Cuts idle time and raises efficiency | Machining centers, CNC milling machines |
| Chucks and fixtures | Hold the workpiece | Control quality and repeatability | Lathes, CNC milling machines |
| Coolant system | Removes heat and clears chips | Extends tool life and improves surface quality | All CNC machines |
| Feedback system | Reports the real axis position | Holds tight tolerances over long runs | Machines built for precision work |
Types of CNC machines
CNC machine types differ in which of the parts above they emphasize. The main components stay the same, but their size and layout change. Different industries lean on different machine types. Choosing among them is a manufacturing decision as much as a design one. The right choice depends on the shape and material of the part. Laser, plasma, and waterjet cutters are also CNC controlled, but they cut sheet and plate by other means. This section focuses on machines that shape parts with cutters, wheels, or sparks.
CNC Milling Machine
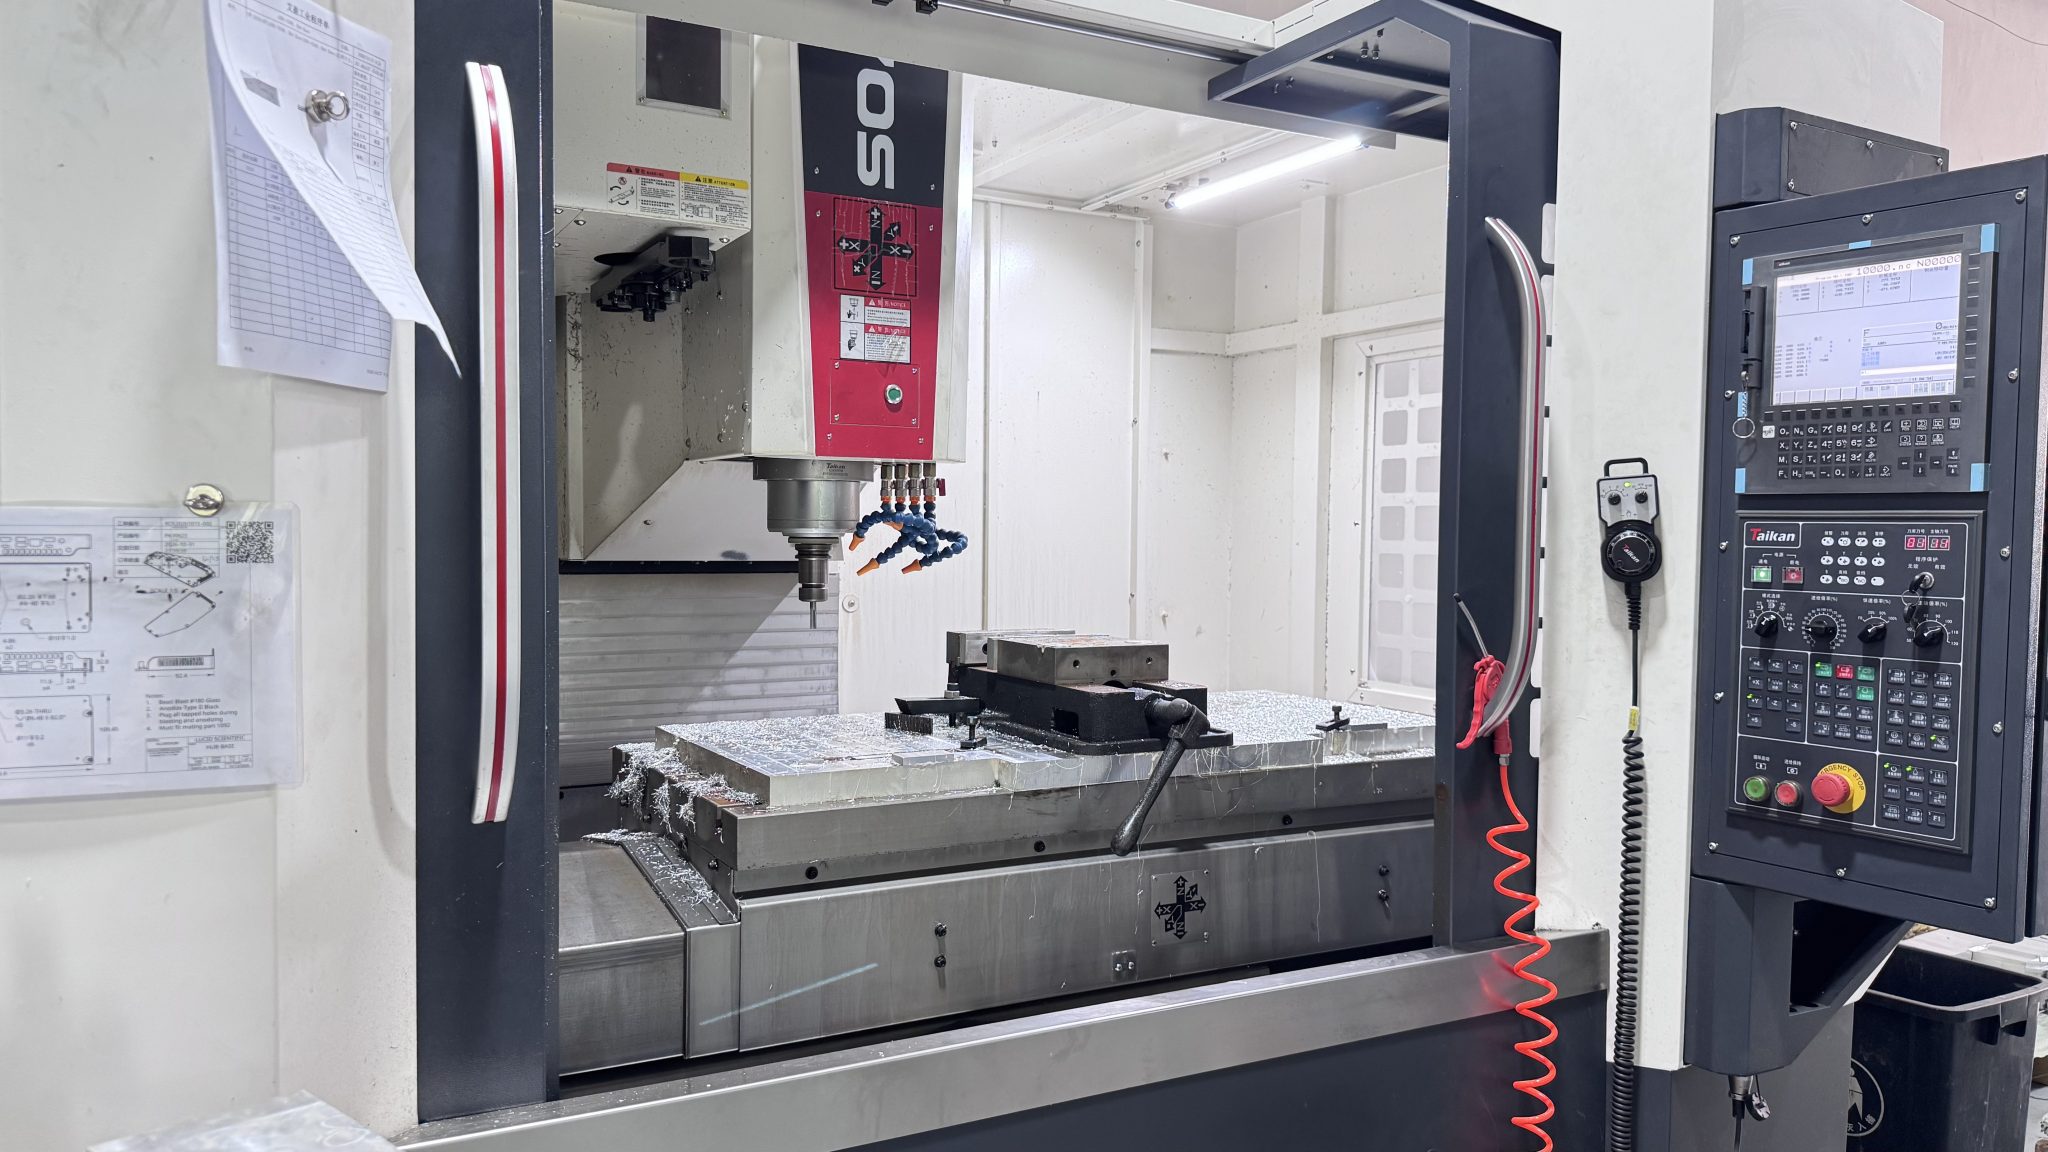
A CNC milling machine uses a rotating cutter to remove material. The part is either held in place or moved under the tool. Milling machines suit flat faces, pockets, slots, holes, and contoured surfaces. The key CNC milling machine parts are the spindle, tool holders, the ATC and magazine, the table, and the axis drives. A rotary table or trunnion can be added when the part needs access from more sides. Because of its versatility, the CNC mill is the first machine many buyers consider.
CNC Turning Machines (Lathes)
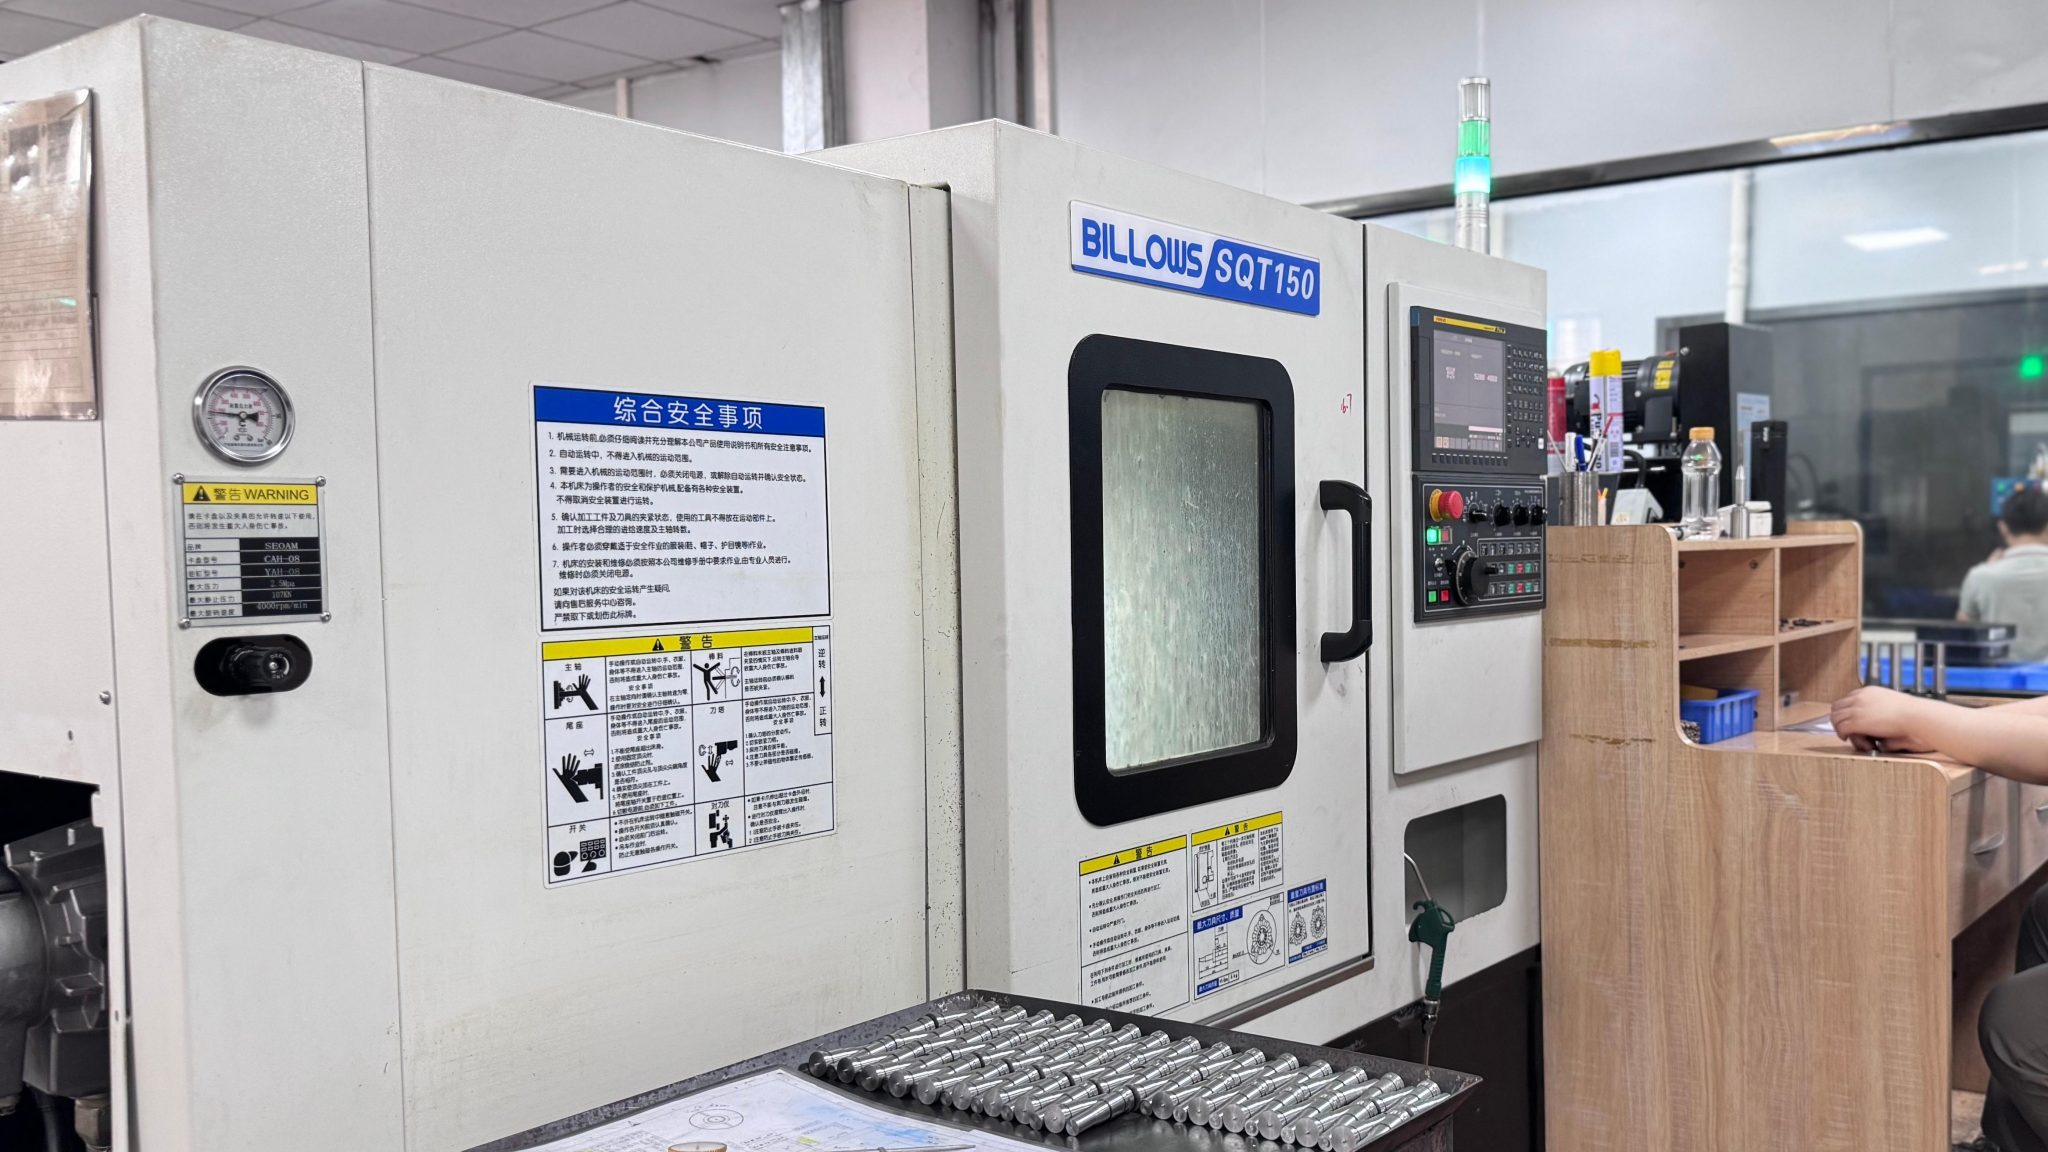
CNC turning spins the workpiece while a stationary tool cuts it. It is efficient for round parts. A CNC lathe makes shafts, pins, bushings, and threaded parts. The headstock, chuck, turret, and tailstock do most of the work.
A turning center adds a turret with live tooling, and often a second spindle. The part can be turned, drilled, and milled in one machine. Then it is handed off to the sub-spindle for the back side.CNC Routers
A turning center adds a turret with live tooling, and often a second spindle. The part can be turned, drilled, and milled in one machine, then handed off to the sub-spindle for the back side.
EDM (Electrical Discharge Machining)
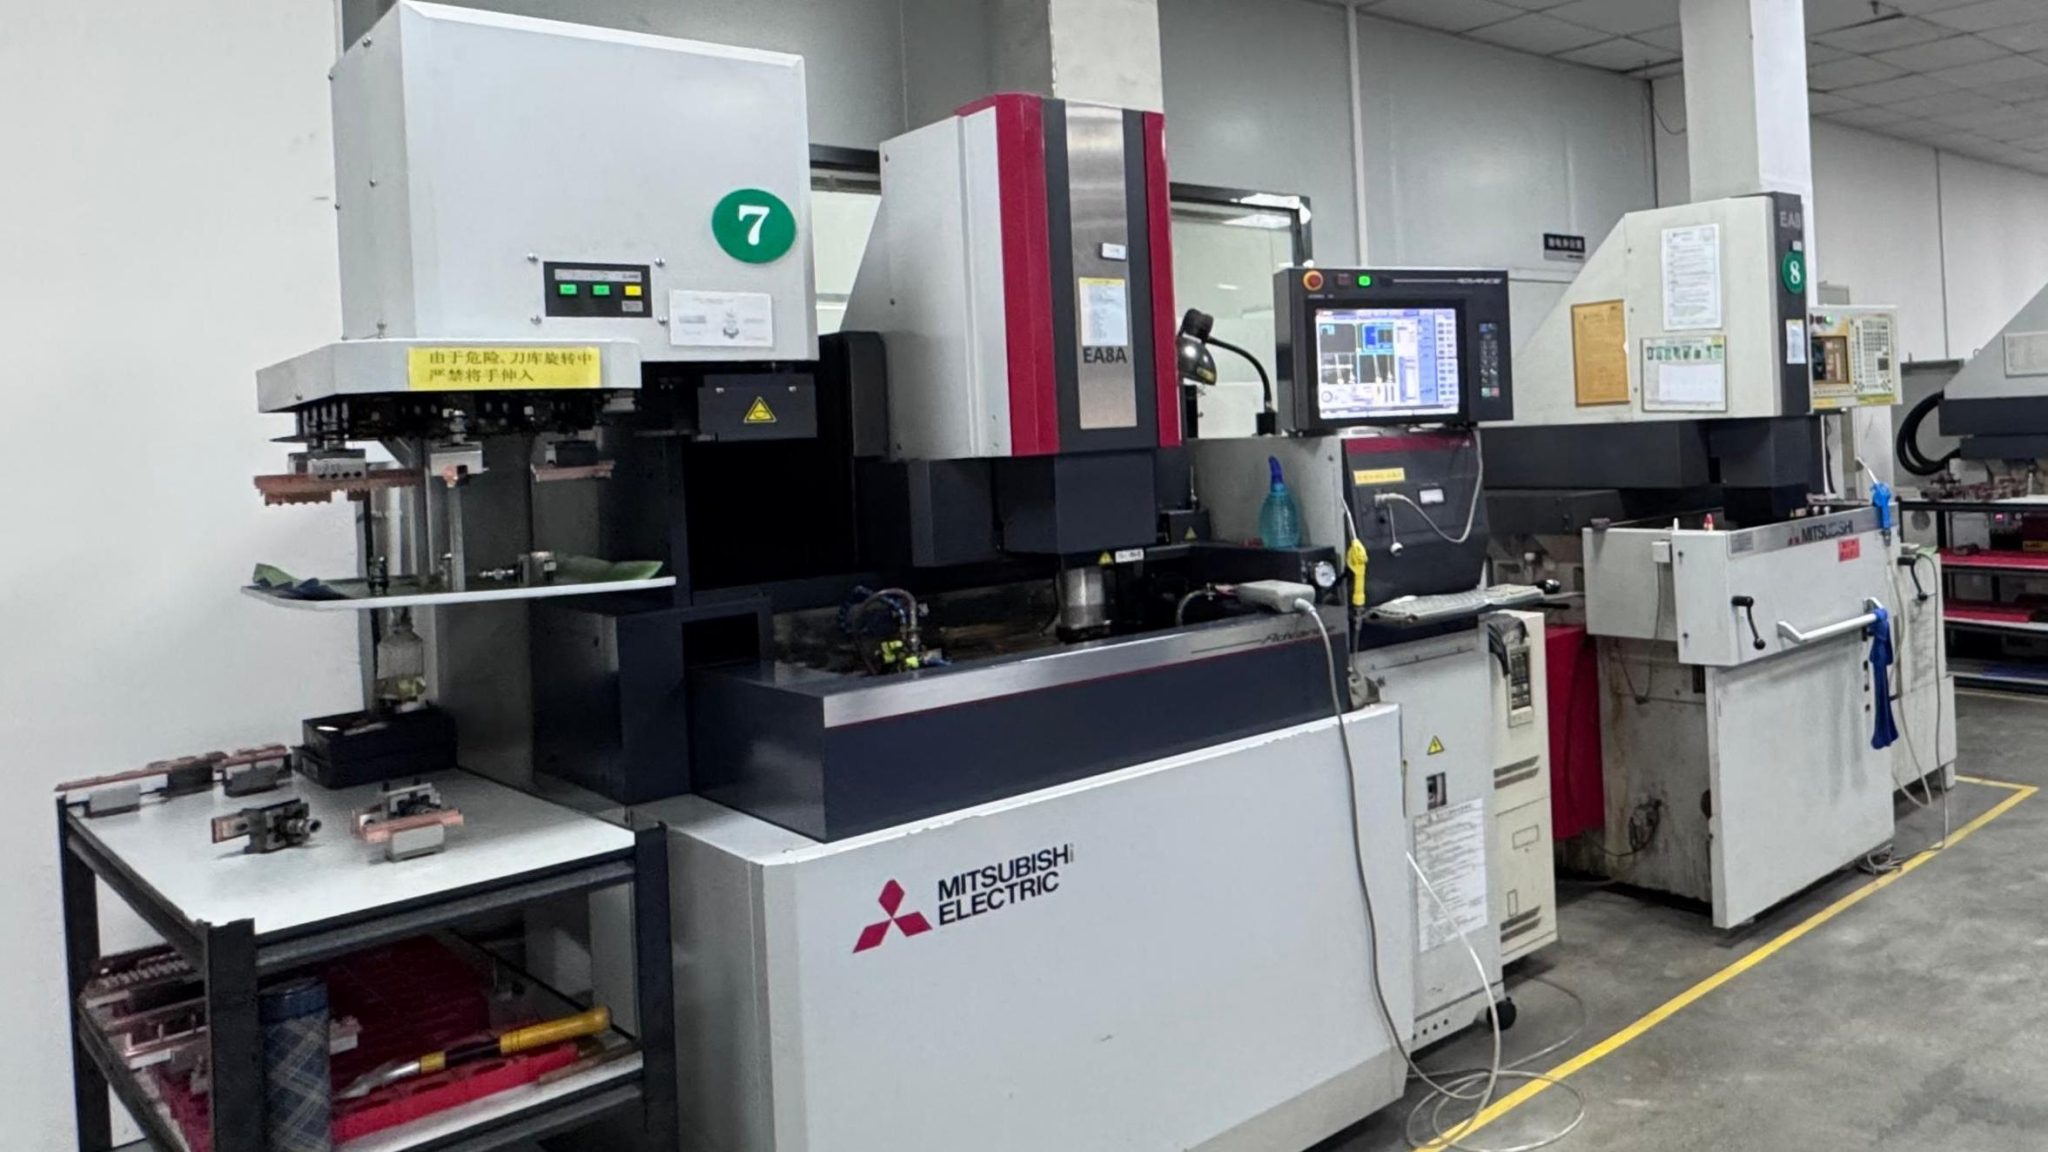
EDM removes material with controlled electrical sparks instead of a cutting tool. It works only on conductive materials. Because there is no cutting force, it handles hardened steel and delicate features that a cutter might bend or break. Mold and die manufacturing relies on it. The trade-off is speed, since it is slower than milling, but the EDM machining process and its variants offer accuracy and geometry options that cutters cannot match.
5-Axis Machining Centers
A 5-axis machining center adds two rotary axes to the three linear ones. It does this with a trunnion table or a tilting head. A 4-axis machine sits in between, with one added rotary axis. Either way, the part needs fewer setups, and the tool can reach angles that a 3-axis machine cannot. These machines are common in the aerospace and medical industries for impellers, blades, implants, and complex housings. The cost is a higher machine rate and more programming effort when compared with more conventional CNC milling processes.
Tips For Getting the Best Results From CNC Machining
Match the part to the CNC machine. This is essential. Look at the dominant shape and features first. Round parts belong on a lathe, where CNC turning processes excel. Boxy parts with pockets and holes belong on a mill. A part with angled faces on several sides may need 5-axis. A hardened part may need grinding or EDM.
Check part size against CNC machine travel. Every CNC machine has a work envelope. A part that is larger than the travel of the axes cannot be cut in one go, no matter how accurate the machine is.
Design for tool access. Cutting tools are round, so inside corners end up with a radius. Use the largest radius the design allows. Deep, narrow pockets need long tools, and long tools bend. Keeping pocket depth modest relative to width gives better accuracy and a lower price.
Apply tight tolerances only where they matter. Higher precision always costs more. Every tight tolerance adds machine time, inspection, and scrap risk. Mark the key features clearly on the drawing and leave the rest at a general tolerance.
Think about how the part will be held. A part needs something to clamp on. Thin walls distort under clamping force, and features cut in a single setup keep their relationships better than features cut across several. The holding method also decides which faces you can reach. If a part needs two setups, say so early and note which datums matter most.
Watch slender and thin-walled parts. They flex under tool pressure. A long shaft may need tailstock support. A thin wall may need lighter cuts or a design change. A small change in proportions can save a lot of machining effort.
Choose materials with machining in mind. Free-machining grades cut faster and wear tools less than tough alloys. Tool wear and cycle time follow the material, and so does cost, which is why many teams rely on custom CNC machining services for metals and plastics to balance material choice with manufacturability.
Ask about equipment and inspection. Find out which machine type will run the job, which machining process it uses, whether probing is used, and how quality and key dimensions are measured. Ask which components matter most for your part. Send the 3D model and the 2D drawing together, and state surface finish requirements on the drawing.
Good manufacturing partners welcome these questions. Aria supports custom parts for engineers and buyers around the world. If you are unsure which process fits a drawing, send it over and the team can review it and suggest an approach
